SELECTION GUIDE · PE FOAM TAPE
PE Foam Tape Thickness: Fill the Gap Without Trading Away Shear Strength
Thickness is usually chosen from the largest gap in the joint. That single number is the wrong input. Here is how to size a double-sided PE foam tape from gap distribution, minimum compression and creep budget instead.
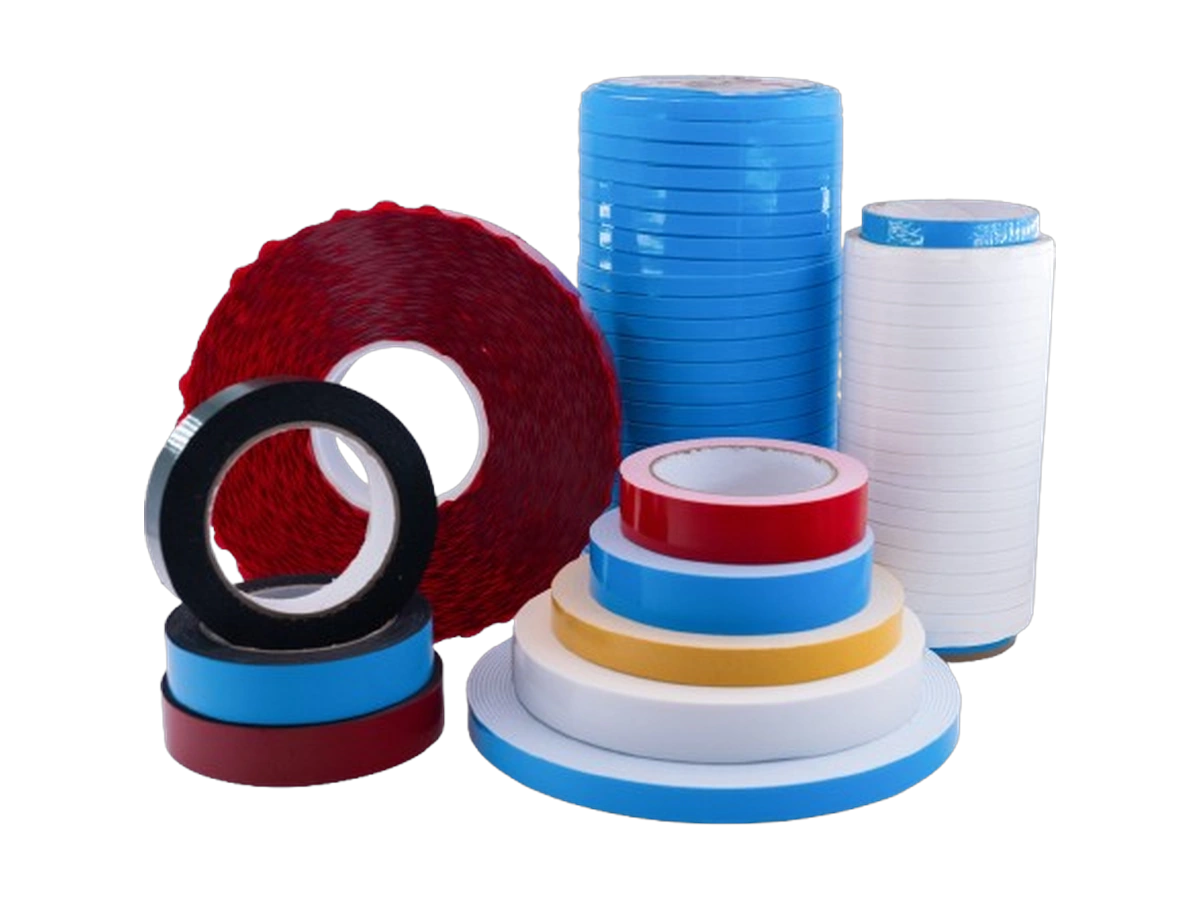
Thickness decisions for PE foam tape are usually made once, early, from a catalogue range — and then never revisited. The inputs that actually govern the choice are rarely collected together: how the gap varies along the bond line, how much compression the joint must retain, and how much sustained load the foam has to resist without creeping. This guide takes them in that order and shows where each number comes from.
The short answer: size for minimum compression, not maximum gap
Most thickness decisions start with the worst gap in the assembly and finish with the thickest tape that covers it. That reasoning inverts the actual constraint. A foam joint has to stay compressed enough to seal and hold, and it has to resist creeping out of that compression over months of load. Both requirements push downward on thickness. Only gap coverage pushes upward.
So the workable question is not which thickness reaches across the widest gap. It is which is the thinnest construction that still keeps every point of the bond line above the minimum compression the joint needs. Everything below that line loses contact. Everything above it buys gap tolerance by spending shear capacity.
- Find the compression floor. Ask the tape supplier for the compression needed to close the joint, expressed as a percentage of nominal thickness, and confirm it against your sealing or handling requirement.
- Characterise the gap as a distribution. Measure across the whole bond line, not at the worst point, and keep the spread.
- Spend the remaining margin on creep, not on comfort. If two thicknesses both clear the compression floor, the thinner one is normally the better engineering choice.
That is the whole method. The sections below explain why each step matters, and where the numbers have to come from.
Why the peak gap is a misleading input
An assembled joint is never one gap. It is a field: stamped panels drift, weld distortion pulls a flange, a moulded rib sinks, powder coating adds 60 to 100 micrometres unevenly, and the fixture that holds the parts during cure loads one end harder than the other. The distance between two mating surfaces therefore varies along the bond line, often by a factor of two or more on the same part.
Choosing thickness from the single largest reading produces a predictable failure. Most of the bond line ends up compressed far beyond the design range, the foam crushes and takes a permanent set, the adhesive at the edges is loaded in peel instead of shear, and the joint lifts at the ends first. Choosing from the average instead produces the opposite defect: the high spots bottom out and carry all the load while the rest of the tape never wets out.
The practical target is the upper part of the distribution, not its extreme. Take the gap at a high percentile across the measured field, then confirm separately that the highest points do not close to zero and stall the tape before the joint seats. That two-part check costs one extra measurement pass and removes most of the thickness risk from the project.
The three constraints that actually set thickness
Thickness is a compromise between requirements that pull in different directions. Writing them down separately stops one requirement from quietly dominating the choice.
| Constraint | What it demands | Direction it pushes thickness |
|---|---|---|
| Gap closure and sealing | Every point of the bond line stays above the minimum compression the joint needs to seal or stay attached | Thicker, where the gap field is wide |
| Load carrying | The foam resists static shear and does not creep out of the joint under sustained load | Thinner, because a thicker foam column has more material available to deform |
| Process and converting | Application pressure can be reached along the whole tape line, and die-cut parts hold tolerance | Thinner, where pressure or access is limited |
Two of the three constraints push toward thinner tape. That asymmetry is why the default instinct to add thickness for safety usually makes a joint worse rather than more robust, and why the choice deserves measurement rather than a rule of thumb.
Thickness and creep: the cost that rarely gets quoted
A PE foam carrier holds a joint apart at a fixed distance and stays elastic while it does so. That elasticity is the product’s value and also its liability. A thicker foam column has a larger volume of compressible material, so under sustained load it has more room to relax, and relaxation shows up as the bonded part drifting, the bond line thinning, or the edge lifting.
Published data sheets for PE foam tapes quantify the effect rather than describe it. A typical construction is rated for a compressive force in the region of 15 to 35 kPa at 25 percent deflection, and states a compression set of roughly 10 to 15 percent after 24 hours at that deflection. In plain terms, a quarter of the compression is spent permanently in the first day and does not come back. If the joint was sized to sit at exactly the minimum compression to begin with, that loss moves it below the sealing threshold.
That is the real mechanism behind edge lift on thick foam joints, and it is not an adhesive failure. The adhesive is still bonded; the carrier underneath it has thinned. It also explains a counter-intuitive result that experienced buyers rely on: for a vertical or overhead load, a thinner foam with a strong acrylic often outperforms a thick, soft foam that looks more substantial.
The BROADYA double-sided PE foam tape range runs from 0.5 mm to 3.0 mm with acrylic adhesive on both faces and a quoted peel of at least 18 N/25 mm, rated across -20 to 120 degrees Celsius. That span is wide enough that picking from the middle of the catalogue is not a selection method. The model-level data sheet for the specific construction, not the family range, is what a specification should cite.
Where the gap field genuinely requires a thick construction, the creep budget has to be bought back somewhere: a denser foam, a larger bond area, mechanical support at the ends of the joint, or a lower sustained load per unit length. Thickness alone cannot supply all three of gap tolerance, load capacity and long-term stability at once. The same trade-off shapes every foam family, which is why the acrylic foam tape selection criteria for industrial assemblies start from load case rather than from carrier thickness.
Measure the gap before the catalogue comes out
The measurement pass is short and it determines everything downstream. What matters is that it captures the distribution, and that it records the conditions the joint will actually see.
- Grid the bond line. Mark measurement points along the full tape path. Ten to twelve points per metre is enough for most assemblies; small parts need at least six.
- Measure the assembled gap, not the loose parts. Read the gap with the parts clamped or fastened in their production sequence. A gap measured before fastening is a different number.
- Record the spread, not just the extremes. Keep the full set. The percentile you size from and the peak you must not bottom out are two different readings from the same data.
- Note what changes with time and temperature. A painted panel measured at 23 degrees Celsius will close up in a hot oven and open in a cold store. If the assembly sees both, the gap field has a range, not a value.
- Write down the load direction. Shear, tensile and peel loading draw on completely different capacities, and only shear makes good use of a foam tape’s thin, wide geometry.
Surface condition belongs in the same record. A gap measured on a release-contaminated moulding is not a gap problem; it is an adhesion problem that a thicker tape will hide for a few weeks. On low-surface-energy plastics such as PP and PE, the adhesive side of the decision has to be settled before thickness is worth discussing, and substrate behaviour on PP and PE surfaces is a separate qualification in its own right.
Validate with dwell time, not with a peel reading
An initial peel test flatters a thick foam tape. The foam is fresh, the adhesive has just wet out, and nothing has relaxed yet. The failure modes this article is about appear later, so the validation has to run later too.
- Read the joint at 24 hours and again at 72 hours. Record bond-line thickness at the measurement points, look for edge lift at the ends of the tape run, and check for any visible slip of the bonded part.
- Load the joint in its service direction. A shear sample and a peel sample on the same construction will rank two candidate thicknesses differently, and only one of those rankings reflects the real assembly.
- Include a temperature excursion. A cycle that takes the joint through the top and bottom of its service range, then returns it to room temperature, exposes differential expansion between dissimilar substrates far more effectively than a static hold.
- Inspect after disassembly. On a failed sample, check whether the foam carrier has thinned permanently while the adhesive is still attached to both surfaces. That signature separates a thickness and creep problem from a contamination problem, and it tells you which variable to change.
Small assemblies justify the same three checks on a shorter timetable. The point is not the duration; it is that the joint gets read after the foam has had a chance to relax. A broader sample validation sequence can be layered on top when the joint also has to survive handling and transit.
What to put in the RFQ
The supplier cannot size a thickness responsibly from a single gap figure, and a specification written from a family data sheet will not survive a qualification review. Six items close most of the gap.
- The substrate pair with surface finish and any coating or release agent, not just material names.
- The measured gap distribution along the bond line, with the percentile the design is sized from.
- The minimum compression the joint needs, and what it is protecting: sealing, retention, vibration isolation or appearance.
- The load per unit length, its direction, and whether it is sustained or intermittent.
- The service temperature range and the number of excursions per year.
- The delivery format, because master roll, slit roll and die-cut parts carry different thickness tolerances and different liner behaviour.
Ask for the model-level compression curve, the compression set figure and the static shear result together. Those three numbers decide the thickness question; peel adhesion alone does not, and a family-level range is not a specification. Where the gap field is wide and the load is real, a short sampling round on production parts will settle in a few days what a catalogue comparison cannot settle at all.
Frequently asked questions
Is a thicker PE foam tape always stronger?
No. Thicker foam adds gap tolerance and vibration damping, and it subtracts static shear resistance because the foam column has more material available to creep. For a sustained vertical load, a thinner, denser construction is frequently the stronger choice in service.
How large a gap can a 3.0 mm PE foam tape bridge?
There is no single figure, because the answer depends on the minimum compression the joint needs. A joint that must stay above 25 percent compression cannot bridge more than roughly three quarters of the nominal thickness in a static condition, and less once compression set and thermal movement are accounted for. Work from the compression floor, then read the gap.
Should the seal prevent water ingress on its own?
A closed-cell PE foam does resist water and air movement, but a foam tape is not a structural sealant and should not be specified as the only barrier in a joint that sees standing water or pressure. Where sealing is the primary function, the foam tape positions and cushions while the sealant or gasket provides the barrier.
Ready to fix a thickness?
Send the measured gap range, the sustained load and the service temperature. Those three decide the construction; peel adhesion alone does not.
- Gap measured at the widest point of the real part
- Load per unit length, with its direction
- Service temperature range, including peaks
Add the substrate pair and target volume, and the team can quote a specific construction instead of a family range.
Send the gap, the load and the substrate
A thickness recommendation is only as good as the joint data behind it. Share the substrate pair, the measured gap range, the load direction and the service temperature, and the team will confirm which construction in the 0.5-3.0 mm range fits.